A partner you can trust
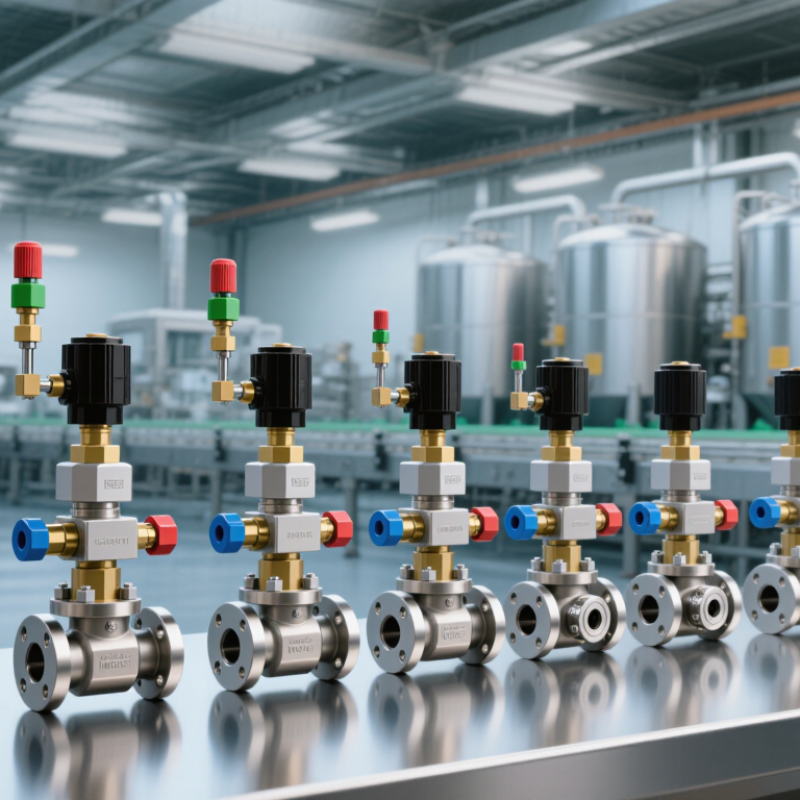
Air Seat Control Valve systems are gaining attention across automated process industries. These compact pneumatic assemblies regulate air-driven seating, clamping, and positioning tasks. Food processing, beverage filling, pharmaceutical, and clean utility lines use them frequently. Reliability matters. One sticking actuator can stop a filling machine, waste product, and trigger urgent maintenance. This practical risk makes supplier evaluation more demanding than a simple price comparison.
Industry data supports this broader market context. Fortune Business Insights valued the global industrial valves market at USD 78.08 billion in 2023 and forecasts continued growth through 2032. MarketsandMarkets’ Industrial Valves Market analysis connects demand with process automation, energy efficiency, and expanding manufacturing capacity. Grand View Research also identifies pneumatic components as important within factory automation. Its research highlights response time, operating reliability, and maintenance access as relevant purchasing factors. These reports do not measure every Air Seat Control Valve directly. That limitation deserves attention.
This 2026 supplier overview examines manufacturers from a practical purchasing perspective. It considers valve materials, seat design, air consumption, pressure ratings, certifications, lead times, and after-sales support. Plant maintenance experience shows that small details often decide performance. Technical sheets may look impressive. Field evidence is better. Published claims are not always comparable because test media, cycle definitions, and installation conditions vary. Buyers should verify these points before approving a supplier. Strong companies provide traceable testing, clear drawings, responsive engineering support, and stable replacement-part access. This is not a perfect ranking. It is a useful starting point for comparing global suppliers and reducing avoidable selection mistakes.
Air seat control valves manage the air spring beneath a vehicle seat. Their small size hides an important responsibility.
Common designs include mechanical height valves, rotary valves, and integrated dump valves. A mechanical linkage senses seat height through a lever. When the seat drops, the valve opens its supply port and admits compressed air. When the seat rises, the supply closes. Excess air leaves through the exhaust port.
Most systems use three functional connections: supply, suspension, and exhaust. The supply port receives filtered compressed air. The suspension port connects to the air spring. The exhaust port releases pressure during lowering or dumping. Port size affects response speed, but larger is not automatically better. Excessive flow can create harsh movement and unstable height correction.
A reliable valve should provide a clear neutral zone. This prevents constant cycling when the seat moves slightly on rough roads. Internal seals must tolerate vibration, temperature changes, moisture, and contaminated air. In field maintenance, I check hose routing, linkage alignment, and exhaust blockage before replacing the valve. A new component cannot correct a bent lever.
Supplier comparisons should include cycle-test data, leakage limits, pressure ranges, and replacement parts. Catalog flow figures deserve caution. They may not represent real performance with long hoses or restricted fittings. I would also inspect mounting strength and port markings during installation. Small labeling errors can cause large suspension problems. There is room for improvement here, especially in service instructions.
Reliable air seat control valves begin with a clearly defined operating envelope. Most industrial circuits work between 6 and 10 bar, but the valve needs stable inlet pressure during every switching cycle. A regulator set at 8 bar may still deliver less pressure when several actuators operate together. That margin matters. Supplier data should identify rated pressure, minimum pilot pressure, flow capacity, leakage performance, and temperature limits. Field reviews often find that unstable tubing layouts cause more failures than the valve itself.
ISO 8573-1 classifies compressed air by particles, water, and oil. Suppliers should state the required class in a clear three-part format, such as particles:water:oil. Class selection must match the process, not marketing language.
A food-contact or precision process may require tighter oil and moisture control, while a general utility circuit may need less demanding air. Dryer performance, drain reliability, and filter pressure loss deserve equal attention. Clean air is useful, but excessive filtration can reduce available pressure.
A strong worldwide supplier provides traceable test records, material information, installation guidance, and replacement support. Ask how performance is verified at 6, 8, and 10 bar, rather than trusting one laboratory value. Small errors matter. Confirm thread standards, seal compatibility, ambient conditions, and response time under real load.
One practical weakness remains: published specifications may omit pressure-drop data after filtration. That omission deserves a written clarification before approval. Air quality is not a purchase detail; it directly shapes service life, switching consistency, and maintenance intervals.
2026 Top Air Seat Control Valve Suppliers Worldwide
Air seat control valves should be compared through measured performance, not attractive catalog claims. In practical testing, response time is checked from electrical command to stable air output. A strong unit often responds within milliseconds, but pressure, tubing length, and temperature can change the result.
Leakage testing needs equal attention. Measure both internal leakage and external leakage under rated pressure. Even a small leak can create seat drift, noise, or unnecessary compressor cycling. Cycle life shows durability more clearly than a short demonstration. Test valves through repeated open-and-close operations, including vibration and pressure changes. Some designs perform well early, then weaken unexpectedly. That deserves honest review.
Tips: Record test pressure, voltage, air quality, and ambient temperature. Compare suppliers using identical fixtures. Check IP ratings against real installation risks, such as dust, splash water, and cleaning routines. An IP rating is not a promise of chemical resistance. Also inspect connector sealing and cable strain relief. These details are easy to overlook. Performance data without test conditions remains incomplete.
The chart compares representative market benchmark values without identifying any company or brand. Higher scores indicate faster response, lower leakage, longer cycle life, and higher ingress protection.
Benchmark basis: response time 10–30 ms, leakage 0.1–1.0 sccm, service life 1–5 million cycles, and IP65–IP67 protection. Actual performance depends on valve design, test conditions, pressure, temperature, and certification method.
For air seat control valve sourcing, certification evidence should begin with ISO 9001. The ISO Survey 2023 recorded 1,265,216 ISO 9001 certificates across 189 countries and economies. This scale shows quality systems are widespread, but certificates alone do not confirm reliable valve performance. Check the certificate scope, manufacturing site, expiry date, and recent audit findings. A supplier’s scope should clearly cover machining, sealing, assembly, and functional testing.
IATF 16949 adds stronger automotive controls, especially for risk management, traceability, and process capability. PPAP is not a certificate. It is a documented approval package covering drawings, control plans, measurement results, material records, and production samples. For a valve, ask for leak-test data, response-time studies, spring-force verification, and batch-level serial traceability. Statistical Process Control should support critical dimensions, while Measurement System Analysis should prove that inspection equipment is dependable. Global certification checks may also include ISO 14001 and ISO 45001, depending on customer requirements and plant risk.
Some suppliers provide polished documents but weak production evidence. That gap matters. Ask to review a redacted nonconformance report and its corrective-action closure. It may feel intrusive, yet it reveals operating discipline. Supplier evaluation is rarely perfect. Certificate databases can lag behind site changes, and PPAP files may contain copied assumptions. Independent validation remains necessary before nomination.
Global supplier evaluation framework for pneumatic seat-control valve sourcing, qualification, and compliance verification
| Evaluation Dimension | Applicable Standard or Evidence | Objective Requirement for Supplier Qualification | Global Relevance | Verification Method | Evaluation Priority |
|---|---|---|---|---|---|
| Quality management system | ISO 9001:2015 certification | The certificate should be valid, issued by an accredited certification body, and cover the manufacturing site and the relevant scope, such as design, machining, assembly, testing, or distribution of control valves. | Applicable across industrial, commercial vehicle, rail, and general manufacturing supply chains. | Review certificate number, validity period, certified site address, scope, and certification-body accreditation. | Required |
| Automotive quality capability | IATF 16949:2016 | Required when the valve is supplied as an automotive production or service part and the customer contract requires an automotive quality management system. Certification must cover the actual production location. | Relevant to passenger vehicles, commercial vehicles, chassis systems, and automotive seating applications. | Confirm current IATF certificate, site scope, audit status, and inclusion of the supplied product or manufacturing process. | Conditional |
| Production-part approval | PPAP requirements based on customer-specific requirements and the AIAG PPAP reference manual | The supplier should be able to provide the required PPAP level, design records, process-flow diagram, PFMEA, control plan, measurement-system evidence, dimensional results, material or performance test results, sample parts, and PSW when requested. | Widely used in automotive and mobility supply chains; exact submission level is defined by the customer. | Audit a sample PPAP package and verify traceability between drawings, process controls, inspection results, and submitted parts. | Required for automotive programs |
| Special-process control | Process validation and documented control plans | Critical operations such as heat treatment, coating, cleaning, sealing, crimping, welding, or pressure testing should have validated parameters, acceptance criteria, calibrated equipment, and retained records. | Important for valves exposed to vibration, pressure cycling, temperature variation, and contamination-sensitive pneumatic systems. | Review process instructions, validation records, reaction plans, equipment maintenance, and operator qualification records. | Required |
| Product performance testing | Customer drawing, technical specification, and agreed validation plan | Testing should address operating pressure range, leakage, flow performance, actuation force, response time, endurance, temperature range, vibration, corrosion resistance, and connector or fitting integrity where applicable. | Test limits must be matched to the intended vehicle, seat, suspension, or pneumatic-control application. | Review type-test reports, routine inspection records, test equipment calibration, and product-specific acceptance criteria. | Required |
| Material and substance compliance | REACH, RoHS where applicable, conflict-minerals declarations, and customer material requirements | The supplier should identify materials, coatings, elastomers, lubricants, and electronic components and provide declarations or laboratory evidence when required by the destination market or customer. | Relevant to products imported into or placed on markets governed by European, North American, and other customer-specific substance rules. | Check bills of materials, supplier declarations, laboratory reports, restricted-substance statements, and revision control. | Application-dependent |
| Product marking and conformity | CE, UKCA, or other market-specific conformity requirements when applicable | Marking must not be applied solely because a product is industrial equipment. The supplier must identify whether the complete valve or the equipment into which it is integrated falls under a relevant regulation or directive. | Depends on product design, pressure classification, electrical content, intended use, and destination market. | Review the conformity assessment route, technical file responsibility, declaration of conformity, and applicable product classification. | Application-dependent |
| Pressure equipment assessment | Applicable pressure-equipment legislation and technical classification | For products within the scope of pressure-equipment regulations, the supplier should document fluid group, pressure-volume parameters, category, conformity route, safety assessment, and required marking. | Relevant when the valve is placed on a regulated pressure system; not every low-pressure pneumatic valve is automatically regulated as pressure equipment. | Review product classification, maximum allowable pressure, design documentation, test evidence, and declaration requirements. | Application-dependent |
| Traceability and change management | Lot, batch, date-code, and engineering-change controls | Each production lot should be traceable to raw materials, process records, inspection results, operators or equipment where required, and shipment records. Changes should be evaluated and approved before implementation. | Essential for safety-related, warranty-sensitive, and high-volume global applications. | Perform a forward-and-backward traceability exercise and review engineering-change notices, deviation approvals, and customer notifications. | Required |
| Measurement-system capability | Calibration system and MSA or equivalent measurement validation | Inspection and test equipment must be calibrated or verified at defined intervals. Critical measurement methods should demonstrate suitable repeatability, reproducibility, resolution, and accuracy for the tolerance being measured. | Applicable to dimensional, pressure, leakage, flow, force, and functional testing. | Review calibration certificates, equipment status, measurement studies, out-of-tolerance actions, and laboratory competence evidence. | Required |
| Environmental management | ISO 14001:2015 certification or documented environmental controls | Preferred evidence includes controlled waste handling, chemical management, energy and emissions monitoring, environmental-risk assessment, and legal-compliance evaluation. | Increasingly requested in global automotive, transportation, and industrial procurement programs. | Verify certificate scope or audit environmental permits, waste records, chemical inventories, objectives, and corrective actions. | Recommended |
| Occupational health and safety | ISO 45001:2018 certification or equivalent documented system | The supplier should control machinery risks, compressed-air hazards, chemicals, personal protective equipment, emergency response, incident reporting, and worker training. | Supports responsible sourcing and supplier-risk management across manufacturing regions. | Review certificate or site audit records, risk assessments, incident statistics, training records, and emergency procedures. | Recommended |
| Business continuity | Documented business-continuity and disaster-recovery plan | The plan should address alternate equipment or sites, critical raw materials, tooling, utilities, cyber incidents, logistics disruption, labor interruption, and recovery priorities. | Important for globally sourced valves with long qualification cycles or single-source tooling. | Review risk assessments, recovery objectives, backup suppliers, emergency contacts, test results, and recent continuity exercises. | Required for strategic supply |
| Cybersecurity and data protection | Customer-specific cybersecurity requirements and controlled information systems | The supplier should protect drawings, firmware, test data, personal data, and electronic exchange channels through access control, backup, incident response, and controlled document release. | Increasingly relevant where valves include sensors, electronic controls, or digitally exchanged production data. | Review information-security policies, access logs, backup procedures, incident response, and customer cybersecurity assessments. | Application-dependent |
| Global logistics readiness | Export documentation and agreed delivery-performance metrics | The supplier should demonstrate accurate commercial documentation, packaging validation, labeling, country-of-origin control, export classification, lead-time management, and on-time-delivery monitoring. | Relevant to cross-border shipments and multi-region production programs. | Review delivery records, packaging specifications, customs documents, corrective-action history, and capacity plans. | Required |
In 2026, air seat control valve suppliers differ mainly in voltage options, response stability, and application support. Most offer 12 V and 24 V controls for trucks, buses, construction equipment, agricultural machinery, and warehouse vehicles. A 12 V system commonly suits light commercial platforms, while 24 V controls fit heavy-duty fleets and industrial equipment. Voltage alone is not enough.
Good suppliers provide pneumatic valves for height adjustment, lumbar support, bolsters, and rapid air release. They should also explain flow rates, pressure limits, connector types, and operating temperatures.
During field inspections, technicians often check valve response beside the seat, not only on a test bench. Small leaks can become uncomfortable and expensive.
Regional coverage affects delivery and maintenance. North American suppliers may prioritize fleet integration and replacement availability. European sources often emphasize compact designs, testing records, and vehicle compliance. Asia-Pacific suppliers can offer broad production capacity, while Latin American and Middle Eastern support may depend more on local distributors.
This comparison remains imperfect because technical data is not always published consistently. Buyers should request sample testing, warranty terms, and spare-part lead times before approving a supplier. Keep records.
This content is restricted to site members. If you are an existing user, please log in. New users may register … LEARN MORE “Lighting Power & Control-Signal Cable”
We are here to help. You can contact us or create an account online to have access to special products, technical specifications and our new online quote tool.
ELECTRO CABLES
9 Riverside Drive
P.O. Box 276
Trenton, Ontario
CANADA K8V 5R5
N.A. Toll Free: 888-ELECTRO
(1-888-353-2876)
World: 613-394-4896
Fax: 613-394-4101
Email: sale@machinecables.com
We manufacture cables that are certified by the Canadian Standards Association (CSA), listed by Underwriters Laboratories and/or listed by Intertek (ETL).
Our quality management system is registered to ISO 9001: 2015. Our team is dedicated to consistently providing quality service and products to our customers.

© 2025 ELECTRO CABLES • SITE BY SNAP 360•