A partner you can trust
Choosing the best Magnetic Hooks for global sourcing requires more than comparing prices or polished product photos. A hook that holds a kitchen towel may fail under warehouse conditions. Another may lose strength after repeated movement. Sourcing decisions should connect magnet strength, hook design, surface protection, packaging, and supplier reliability.
Begin with the intended application. Define the load, contact surface, temperature range, and expected usage frequency. A hook for office partitions differs from one used on steel shelving. Request measured pull-force data, material details, coating information, and dimensional drawings. Sample testing matters. Place each sample on the actual target surface, then test vertical and sideways loads. Record results with simple photographs and repeat the test after several days.
Small details reveal supplier competence.
Global sourcing also requires disciplined supplier evaluation. Review production experience, quality-control procedures, batch consistency, and export packaging. Ask how the supplier handles scratches, weak magnets, loose hooks, and mixed cartons. Independent inspection can verify quantities and basic specifications before shipment. Relevant product documentation should be checked for the destination market and intended use. Requirements may differ between countries, so local compliance advice remains valuable.
The cheapest option is rarely the safest choice. However, the most expensive hook is not automatically the best. A practical comparison should include unit cost, tooling, packaging, shipping volume, defect risk, and replacement costs. Some assumptions will be wrong. That is normal. Strong sourcing teams test those assumptions early and revise the specification when evidence changes. Reliability grows through careful questions, documented tests, and honest supplier communication.
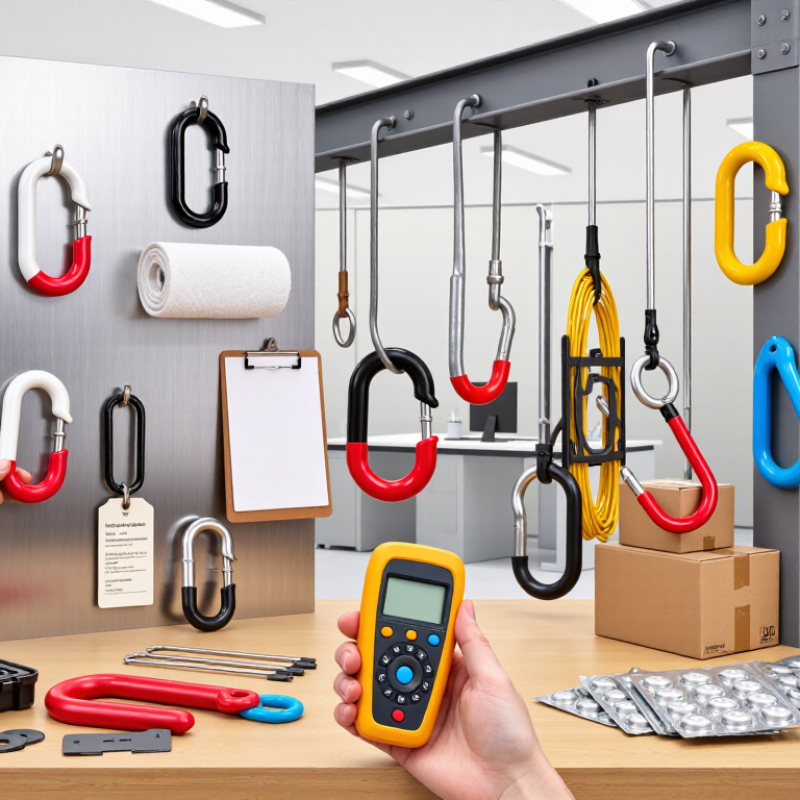
Magnetic hooks come in several practical forms. Cup-base hooks suit flat steel panels and offer strong vertical holding power. Swivel hooks rotate, helping cables or tools hang at different angles. Covered hooks protect painted surfaces, while compact disc hooks fit narrow storage areas. Select the type according to the mounting surface, load direction, and available space.
Pull-force ratings require careful reading. Manufacturers may list force in Newtons (N) or kilograms-force (kgf), not ordinary kilograms. One kilogram-force equals about 9.81 N. Therefore, a 100 N rating equals roughly 10.2 kgf under ideal testing. It does not guarantee a 10.2-kilogram load in daily use. Testing usually involves a clean, thick steel plate and a direct pull. Paint, rust, air gaps, and sideways loading can reduce performance sharply. Ask suppliers for test conditions, magnet grade, surface thickness, and inspection records.
In practical sourcing, apply a safety margin of two or three times the working load. A 10-kilogram hanging load may need a hook rated near 196–294 N, depending on movement and impact. Check the hook after installation. It should not slide when gently pulled sideways.
I once underestimated a thin steel cabinet door; the rated hook held, but the door flexed. The specification was accurate, yet my application judgment was weak. That lesson matters when comparing samples from different factories. Small details often decide real-world reliability.
Neodymium grades deserve careful comparison. N35, N42, and N52 describe magnetic energy, not guaranteed hook capacity. A higher grade may provide stronger pull in a compact hook. However, the steel surface, air gap, hook design, and pulling direction also matter. Ask suppliers for tested holding force, working temperature, and safety factors. Catalog numbers alone are not enough.
Coating choice affects service life. Nickel-copper-nickel coatings suit dry indoor environments and offer a hard, familiar finish. Epoxy coatings can provide better moisture protection, but scratches may expose the magnet beneath. Zinc coatings are economical, yet they may not suit persistent humidity. Review coating thickness and edge coverage closely. Small gaps around a hook can become corrosion starting points.
ASTM B117 results help compare corrosion resistance under controlled salt fog. The test commonly uses a 5% salt solution at about 35°C. Request exposure hours, visible rust criteria, blister ratings, and photographs of tested samples. Test the complete hook assembly, not only loose magnets. A long salt-spray result does not predict every outdoor environment. I have seen sourcing decisions rely on one impressive number. That is risky. Verify batch traceability, repeat testing, and packaging protection. No coating is perfect. Moisture can still enter through damaged edges.
A strong magnetic hook needs more than an impressive holding-force number. In practical sourcing, ask whether the force applies to a clean, thick steel plate or a painted, curved surface. Air gaps, rust, heat, and sideways loading can reduce performance sharply. A small washer or uneven contact may also change the result. Test it.
Use a 3:1 design factor when setting the safe working load. If a hook fails at ninety kilograms under a defined test, its working load should not exceed thirty kilograms. This is a design safeguard, not a universal legal requirement. Confirm whether the test measures vertical pull, shear, shock, or repeated loading. These forces behave differently.
Never rely on a catalog figure without test conditions, sample identification, and batch records. A clean laboratory plate can mislead.
ISO 12100 supports a structured machinery risk assessment, rather than a simple product label. Identify hazards such as dropped objects, pinch points, sharp edges, magnet detachment, and unexpected movement. Reduce risk through safer geometry, suitable materials, secure attachment, and clear use instructions. Then address remaining risks with warnings and training.
Ask suppliers for documented risk controls, inspection procedures, material data, and traceable test reports. I would question any supplier offering only a polished photograph. That feels incomplete. Even a careful specification can miss corrosion, temperature cycling, or user error, so independent verification remains worthwhile.
How to Choose the Best Magnetic Hooks for Global Sourcing?
A reliable supplier should provide current RoHS and REACH documentation for each magnetic hook model. RoHS evidence should address restricted substances in coatings, plastics, solder, and metal parts. REACH checks chemical obligations, including substances of very high concern. Do not accept a generic certificate without product references. Ask for laboratory reports, issue dates, test methods, and sample identification.
ISO 9001 matters differently. It confirms a quality management system, not automatic product compliance. Request the certificate scope and verify whether manufacturing, inspection, and corrective actions are covered. During supplier screening, review incoming material records, magnet pull-force tests, coating inspections, and batch traceability. A factory may show strong paperwork yet struggle with consistent hook alignment.
Test samples under realistic conditions. Mount them on painted steel, apply the stated load, and leave them overnight. Check slipping, surface marks, corrosion, and hook rotation. Keep photographs and measured results. Small details matter.
I once overlooked packaging pressure during evaluation. Several hooks arrived with scratched coatings, although the production samples looked excellent. That mistake changed the checklist. Ask how magnets are separated, how cartons are sealed, and how damaged units are recorded. Require a pre-shipment inspection and a corrective-action process. Supplier answers should be specific, dated, and supported by records, not confident promises.
| Screening Dimension | Requirement or Benchmark | Evidence to Request | Verification Method | Screening Result |
|---|---|---|---|---|
| Product Definition | Confirm hook dimensions, magnet type, surface finish, thread or attachment design, and intended load direction. | Technical drawing, product specification sheet, material declaration, and approved sample. | Compare the drawing with the physical sample and purchase specification. | Pass if all critical dimensions and materials are documented. |
| Magnetic Holding Force | Use a defined test condition; holding force varies with steel thickness, air gap, contact area, load direction, and surface condition. | Test procedure, measured values, fixture details, and safety factor used for the rated load. | Repeat the test on production samples using the same steel plate, air gap, and pull direction. | Pass only when the stated load is supported under defined conditions. |
| RoHS Substance Control | For homogeneous materials, restricted substance limits include 0.1% for lead, mercury, hexavalent chromium, PBB, PBDE, DEHP, BBP, DBP, and DIBP; cadmium limit is 0.01%. | Current RoHS declaration, homogeneous-material breakdown, and laboratory test report where applicable. | Check report scope, sample identity, test date, laboratory details, and results against the applicable restricted-substance limits. | Pass when all applicable materials meet the stated limits or a valid exemption is documented. |
| REACH Candidate List | If a Candidate List substance is present in an article above 0.1% by weight, communication duties may apply; additional obligations can depend on market and annual quantities. | REACH material declaration, current Candidate List review, and article-level substance information. | Review each material, coating, adhesive, and packaging component separately; verify the declaration date. | Pass when substance content and required communication information are complete and current. |
| Coating and Plating Safety | Coating must resist normal handling, humidity, abrasion, and corrosion without exposing the magnet or hook material prematurely. | Coating specification, adhesion results, corrosion test method, and surface-finish inspection standard. | Inspect for blistering, peeling, rust, sharp edges, and exposed substrate after defined testing. | Pass when finish performance matches the intended environment. |
| ISO 9001 Certification | The supplier should hold a valid ISO 9001 certificate covering the relevant manufacturing activities and site. | Certificate number, issuing certification body, covered site, scope, issue date, expiry date, and audit status. | Verify the certificate directly through the certification body or an authoritative certification database. | Pass only if certificate status, site, scope, and validity are confirmed. |
| Quality-Control Plan | Controls should cover incoming materials, magnetization, dimensions, appearance, holding force, packaging, and final release. | Inspection plan, sampling standard, calibrated equipment list, and sample inspection records. | Audit the process flow and compare records with the agreed product specification. | Pass when controls are documented, repeatable, and traceable to batches. |
| Traceability | Each shipment should be traceable to production date, raw materials, inspection records, and packaging units. | Batch-code format, production records, material certificates, and retention policy. | Select a shipment code and trace it backward to material and inspection documentation. | Pass when one-step-back and one-step-forward traceability is demonstrated. |
| Packaging and Transport | Packaging should prevent scratching, demagnetization risk from unsuitable handling, corrosion, and contact damage during international transport. | Packing specification, carton labeling, moisture protection plan, and transport test records when available. | Review packaging samples and conduct handling, stacking, and unpacking inspections. | Pass when packaging protects product quality and supports customs identification. |
| Supplier Approval Decision | Approve only after technical, compliance, quality-system, sample, and commercial reviews are complete. | Completed supplier questionnaire, signed specification, compliance file, audit report, and corrective-action records. | Use a documented approval checklist with mandatory evidence for RoHS, REACH, and ISO 9001. | Conditional approval if any mandatory evidence remains incomplete. |
Note: Compliance status should be confirmed against the regulations and Candidate List applicable to the destination market at the time of purchase.
How to Choose the Best Magnetic Hooks for Global Sourcing?
Calculate Landed Cost, MOQ, Incoterms, Lead Time, and 2% Defect Targets
A dependable comparison starts with landed cost, not unit price. Add the hook, magnet, packaging, inland transport, freight, insurance, duties, brokerage, inspection, and payment fees. A quote of $0.42 may become $0.71 after delivery. Request a cost sheet with currency, validity, and shipment assumptions. Check whether the Incoterm is EXW, FOB, CIF, or DAP. These terms allocate transport responsibilities, but they do not guarantee quality.
MOQ can change the decision quickly. Ask for pricing at 500, 2,000, and 10,000 pieces. Then calculate inventory cash and storage space. A lower MOQ may cost more, but it can reduce unsold stock. Lead time should include sampling, approval, production, inspection, and port delays. Get each stage in writing. Add a realistic buffer. Delays happen.
Test the magnetic hook on the actual surface. Painted steel, stainless steel, and uneven doors can produce different holding strength. Specify load direction, coating, temperature, and corrosion requirements. Set a 2% defect target with a clear inspection method and corrective-action deadline. Do not accept “good quality” as a standard. Review samples, test reports, packaging photos, and independent inspection records. I would still question a perfect forecast. Early estimates often miss customs delays or damaged cartons. A small pilot order can expose those weaknesses before full production.
This content is restricted to site members. If you are an existing user, please log in. New users may register … LEARN MORE “Lighting Power & Control-Signal Cable”
We are here to help. You can contact us or create an account online to have access to special products, technical specifications and our new online quote tool.
ELECTRO CABLES
9 Riverside Drive
P.O. Box 276
Trenton, Ontario
CANADA K8V 5R5
N.A. Toll Free: 888-ELECTRO
(1-888-353-2876)
World: 613-394-4896
Fax: 613-394-4101
Email: sale@machinecables.com
We manufacture cables that are certified by the Canadian Standards Association (CSA), listed by Underwriters Laboratories and/or listed by Intertek (ETL).
Our quality management system is registered to ISO 9001: 2015. Our team is dedicated to consistently providing quality service and products to our customers.
© 2025 ELECTRO CABLES • SITE BY SNAP 360•