A partner you can trust
A Stainless Steel Coil Manufacturer produces wide, continuous strips of stainless steel for construction, automotive, food-processing, and industrial applications. The process begins with carefully selected slabs, followed by hot rolling, cold rolling, annealing, pickling, and finishing. Each stage changes the coil’s thickness, surface, strength, and corrosion resistance. These details matter when a coil will become a kitchen panel, pressure vessel, or precision component.
Experienced manufacturers do more than operate rolling mills. They review material grades, dimensional tolerances, surface requirements, and end-use conditions before production begins. Their technical teams monitor furnace temperatures, rolling pressure, edge quality, and coil shape. Testing may include chemical analysis, hardness checks, tensile testing, and visual inspection. Traceable records connect each coil to its production batch. That evidence supports dependable purchasing decisions.
Quality is visible in practical details. A finished coil should unwind smoothly, show consistent width, and maintain a clean surface under proper lighting. Packaging also matters. Strong supports, moisture protection, and clear labels can prevent damage during storage and transport. However, no factory is flawless. Small variations can appear between batches, especially when specifications are unclear or inspections are rushed. A trustworthy supplier acknowledges these risks and explains them plainly. Buyers should ask for test certificates, inspection procedures, production experience, and realistic delivery information. This article examines how a Stainless Steel Coil Manufacturer works, what separates capable producers from ordinary suppliers, and how technical evidence can guide a safer, more informed selection. Guesswork is expensive.
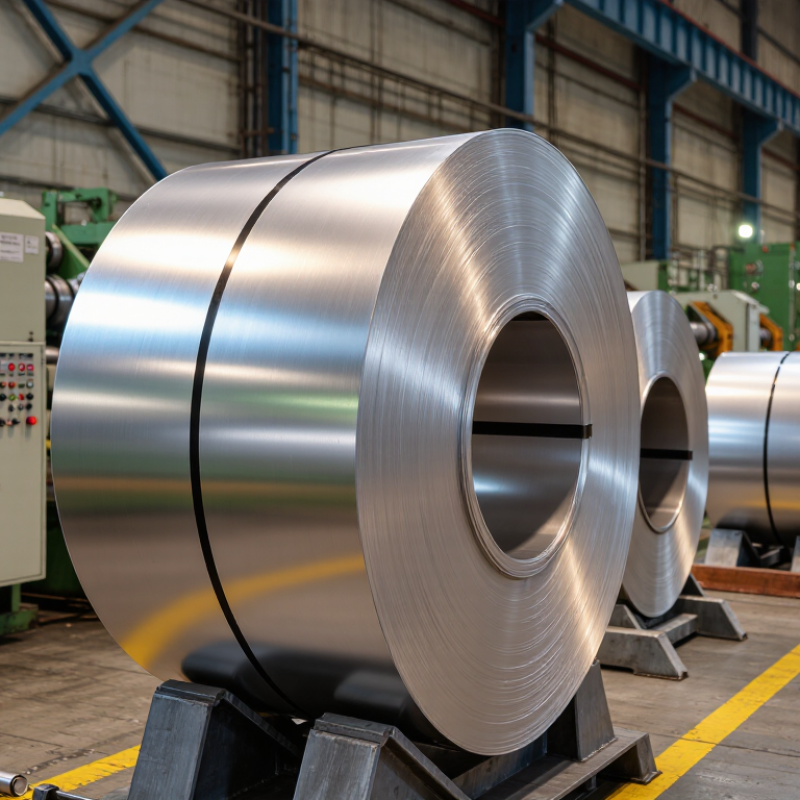
A stainless steel coil manufacturer converts raw materials into rolled, inspected, and traceable metal coils. Its work usually begins with melting and refining, followed by continuous casting, hot rolling, cold rolling, annealing, and pickling. Some facilities also provide slitting, leveling, edge trimming, and surface finishing.
The scope is wider than production alone. Manufacturers manage grades, thicknesses, widths, surface finishes, tolerances, packaging, and delivery schedules. They also issue mill test certificates and maintain heat-number traceability. In practical use, buyers may inspect coil edges, flatness, surface marks, and winding tension before fabrication. Small defects can create large losses during stamping or tube forming.
The International Stainless Steel Forum reported 58.4 million tonnes of global stainless crude steel production in 2023. That figure shows the industry’s scale, but it does not measure manufacturing quality by itself. Quality depends on process control, testing, and honest documentation. ASTM and EN requirements often guide chemical analysis, mechanical testing, dimensions, and surface condition. Yet standards are not always interpreted identically. This is where experienced technical communication matters. A capable manufacturer should clarify the application, not merely quote a grade. It should explain limitations, lead times, and inspection methods before shipment. Some suppliers may call themselves manufacturers while only cutting or reselling coils. The boundary is not always clear. Checking production certificates, facility capabilities, and independent inspection records remains sensible.
A stainless steel coil manufacturer converts steelmaking inputs into flat-rolled, continuously wound products. Its core functions include melting and refining, casting, hot and cold rolling, annealing, pickling, finishing, inspection, and coil packaging.
Chart interpretation: Chromium provides stainless steel’s basic corrosion resistance, while nickel supports austenitic structures and improves toughness. The figures show representative specification limits for commonly used coil grades and are not company-specific production data.
A stainless steel coil manufacturer begins with controlled raw materials, not with rolling equipment. Steel becomes stainless when chromium reaches at least about 10.5%, allowing a protective oxide film to form. That film is thin but remarkably effective. It can repair itself when oxygen is available. Nickel, molybdenum, carbon, and nitrogen then adjust strength, formability, and corrosion resistance. Small details matter.
Grade 304 is widely used for kitchen equipment, tanks, and general fabrication. It usually contains around 18% chromium and 8% nickel. Grade 316 adds molybdenum, often near 2–3%, improving resistance to chlorides and salt exposure. However, 316 is not immune to corrosion. Surface contamination, poor cleaning, and stagnant water can still create problems. That point is sometimes overlooked.
Duplex steel combines austenitic and ferritic structures. It commonly offers higher strength than 304 or 316, with useful resistance in demanding environments. Its production requires careful control of heat treatment and cooling. A coil manufacturer should verify chemical composition, mechanical properties, thickness, surface finish, and heat-number traceability. Mill certificates help, but a certificate alone is not enough. Independent testing may reveal variation between batches. The difficult part is resisting convenient assumptions. One grade may fit several applications, yet the correct choice depends on temperature, chloride levels, forming requirements, welding, and maintenance conditions.
A stainless steel coil manufacturer converts raw materials into controlled, usable strip. The process starts with melting iron, chromium, nickel, and other alloying elements in an electric furnace. Chemical analysis checks chromium content and carbon levels before casting. According to the International Stainless Steel Forum, global stainless crude steel production reached about 58.4 million tonnes in 2023. That figure shows the scale of this industry, but not every coil has identical performance.
Hot rolling reduces the cast slab into a thinner coil. Cold rolling then improves thickness accuracy and surface finish. Annealing heats the strip to restore ductility after rolling. Pickling removes oxide scale and heat tint, often leaving a clean metallic surface. Slitting cuts the wide coil into narrower widths, using adjusted knives and tension controls. A small setup error can create burrs, edge waves, or uneven winding. Some variability remains. Experienced manufacturers inspect each stage instead of trusting one final test.
Tips: Check the mill certificate, surface condition, thickness tolerance, and coil weight. Ask whether pickling was completed after annealing. Confirm slitting width and edge quality with actual samples. The World Steel Association notes that steel production carries significant energy and emissions demands, so material yield and process efficiency deserve attention. A reliable supplier should explain these controls clearly, provide traceable records, and admit when a specification needs review.
A stainless steel coil manufacturer does more than slit and ship metal. It controls chemistry, thickness, surface, heat treatment, and documentation from melt to dispatch. The International Stainless Steel Forum reported 58.4 million tonnes of crude stainless steel production in 2023. At that scale, small process errors can multiply quickly. A reliable supplier links each coil to a heat number, test report, and inspection record.
ASTM A240/A240M sets requirements for chromium and chromium-nickel stainless sheet, strip, and plate. Gauge control starts with calibrated micrometers, repeated across width and length. ASTM A480/A480M also supports general tolerance and finish requirements. Surface checks should use controlled lighting, not casual warehouse judgment. Operators inspect for pits, roll marks, scratches, edge cracks, and discoloration. Chemistry requires more than a grade label. Optical emission spectroscopy can verify chromium, nickel, molybdenum, manganese, carbon, and nitrogen. Positive material identification adds a practical cross-check.
ISO 9001 strengthens the system around these tests. ISO’s 2023 Survey records more than one million ISO 9001 certificates worldwide, but certification alone proves no coil’s quality. It shows a managed process. The manufacturer still needs calibration records, nonconformance control, corrective actions, and retained samples. This is where experience matters. A polished surface can hide a thickness problem. A correct gauge can still carry unstable chemistry. Inspection plans should be questioned when sampling is too light or drawings are vague. Perfect control is an ambition, not evidence.
A stainless steel coil manufacturer produces, processes, and inspects continuous steel strips for industrial use. In practice, specification control matters more than attractive catalog language. Thickness may range from 0.3 to 6 mm, depending on the application. Thin coil suits formed panels and precision components. Heavier coil supports structural parts and demanding fabrication.
Width must match the customer’s cutting plan. Common requests include narrow slit coils, standard widths, and custom dimensions. A small width error can increase scrap during stamping. Edge condition also deserves careful attention. Mill edges may retain the original rolled profile, while slit edges are cut lengthwise. Burrs, waviness, or uneven edges can affect feeding and welding.
Surface finish changes both appearance and performance. A bright finish may suit visible panels, while a brushed finish can reduce reflections and hide light handling marks. A matte surface may improve visual consistency in equipment housings. Manufacturers should record roughness, inspection methods, and tolerance ranges clearly. They should also provide traceable test documents for chemistry, mechanical properties, and dimensional checks.
Real production is rarely perfect. Coil shape can shift slightly after slitting or transport. Even experienced buyers sometimes focus on thickness and overlook edge quality. That mistake can become expensive. Request sample material, confirm the full specification, and review how the manufacturer controls each batch.
This content is restricted to site members. If you are an existing user, please log in. New users may register … LEARN MORE “Lighting Power & Control-Signal Cable”
We are here to help. You can contact us or create an account online to have access to special products, technical specifications and our new online quote tool.
ELECTRO CABLES
9 Riverside Drive
P.O. Box 276
Trenton, Ontario
CANADA K8V 5R5
N.A. Toll Free: 888-ELECTRO
(1-888-353-2876)
World: 613-394-4896
Fax: 613-394-4101
Email: sale@machinecables.com
We manufacture cables that are certified by the Canadian Standards Association (CSA), listed by Underwriters Laboratories and/or listed by Intertek (ETL).
Our quality management system is registered to ISO 9001: 2015. Our team is dedicated to consistently providing quality service and products to our customers.
© 2025 ELECTRO CABLES • SITE BY SNAP 360•